Wire Cut EDM Machine
Fast-wire and precision medium-wire EDM cutting built for die plates, punches and mould inserts — a CNC wire cut EDM machine with published tolerances, taper data and a straight answer on lead time. As a cnc wire cut machine it is judged on the cast bed and the pulse supply, not on the table size alone.
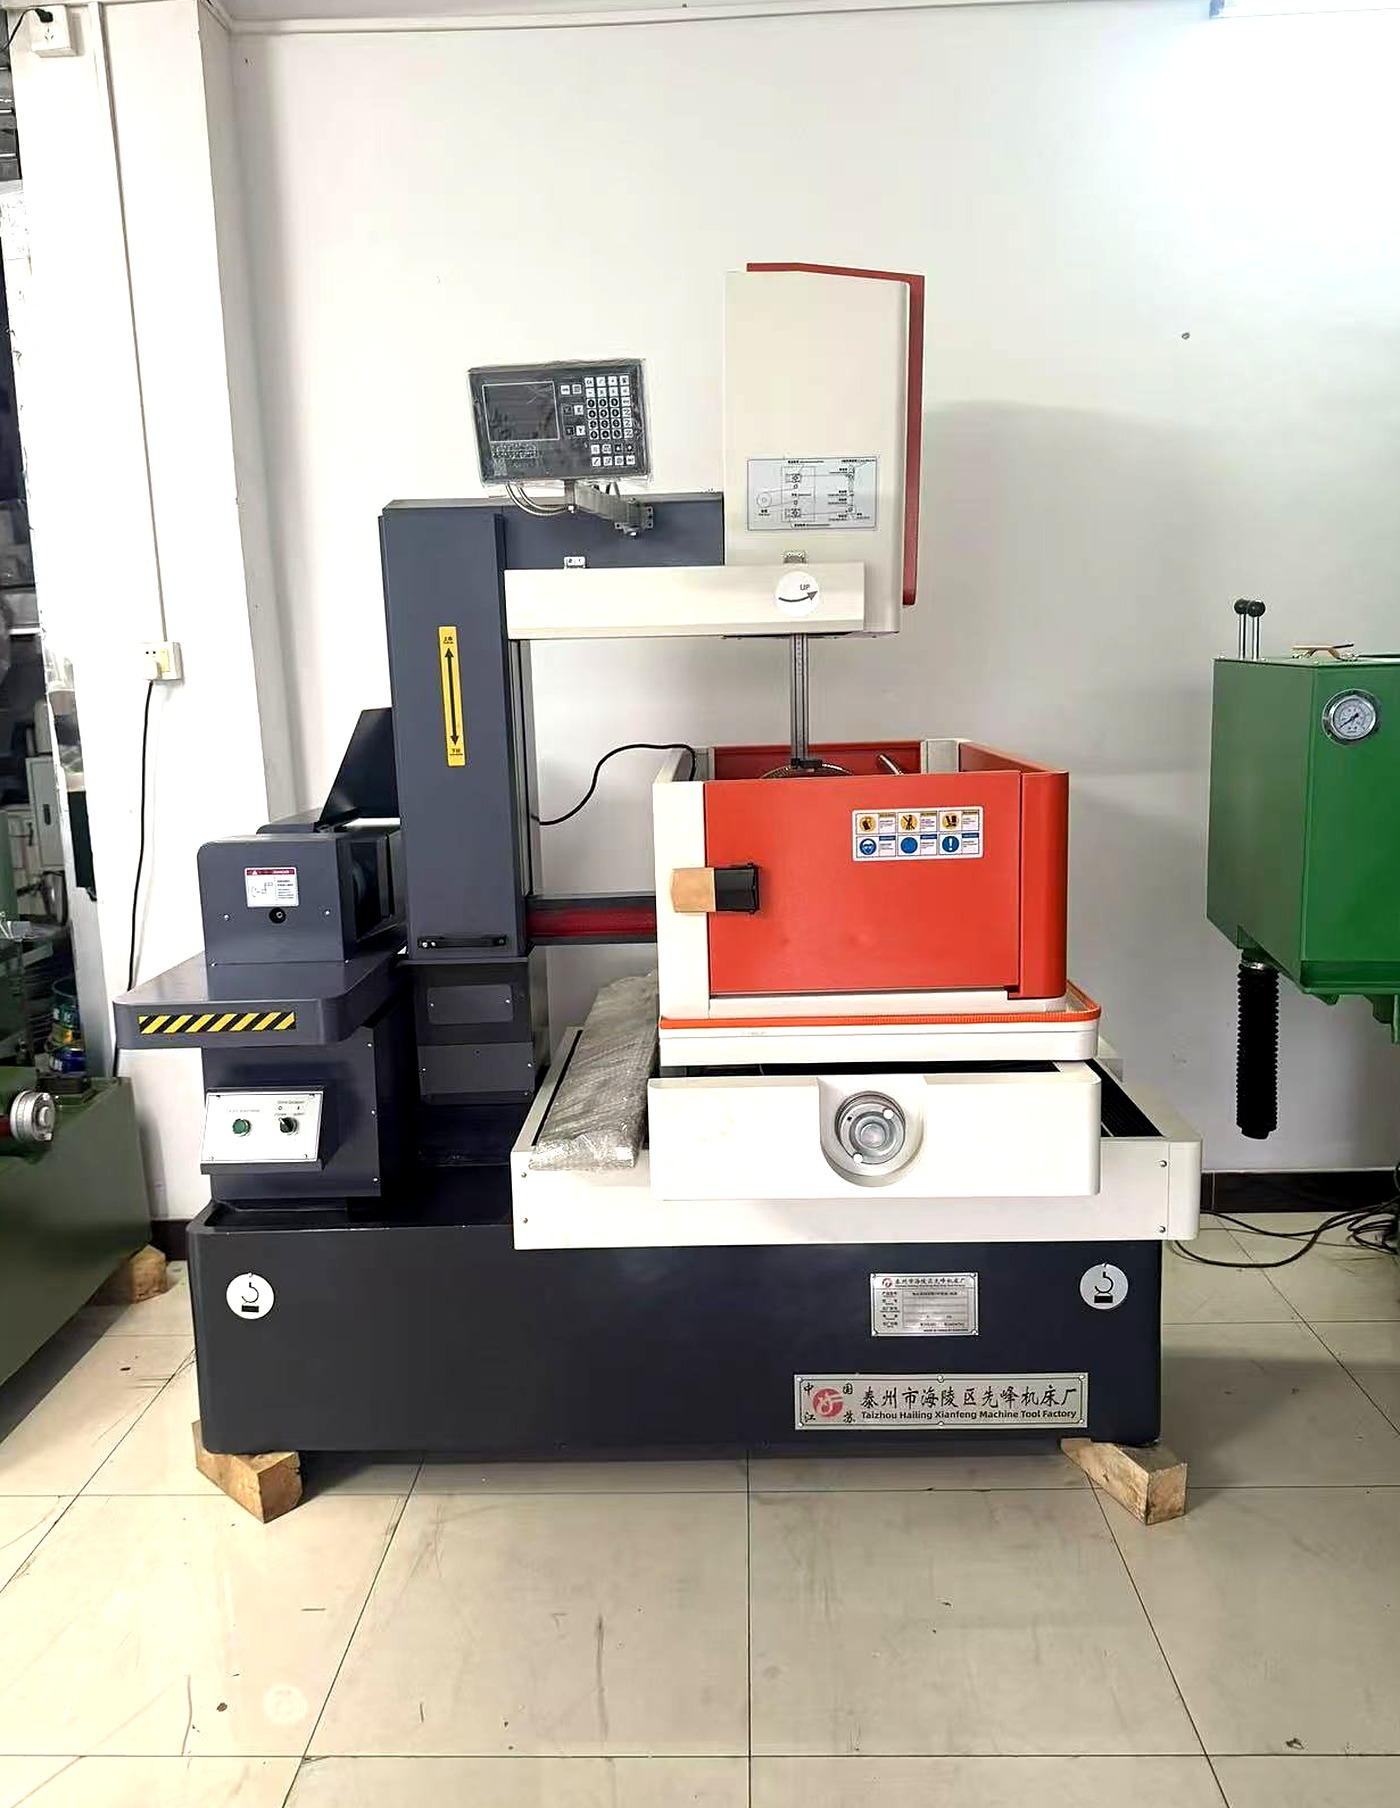
Wire cut EDM machine built to your tolerance
Wire EDM cuts conductive metal with a thin wire electrode and a controlled spark, so the part is cut without tool force — hardened die steel, thin walls and delicate profiles all machine the same way. What separates our models is not the principle, it is how the wire is handled: a single fast pass, or several controlled skim passes. That handling is what decides EDM surface roughness: a single fast pass lands around Ra 2.5-3.0 µm, while multi-pass skimming on the medium-wire machine reaches Ra 1.2 µm. Wire cut electrical discharge machining removes metal by spark erosion rather than by a cutting edge, which is why an EDM spark machine can cut hardened steel that a milling cutter cannot reach.
Tell us the plate thickness, the tolerance and the finish you need on the drawing, and we will point you to DK7735, DK7745 or TLBJ-40TC — rather than quoting the largest machine and leaving you to pay for capacity you will not use. The wire cutting machine price we quote is for that configuration, not for a stripped base unit.
Fast wire vs. medium wire
One pass, economical
Molybdenum wire running at high speed, reused across the job. Suited to general die work where Ra 2.5–3.0 µm is acceptable.
• DK7735 — 450 × 350 mm travel
• DK7745 — 550 × 450 mm travel
• Both cut up to 400 mm depth
Multi-pass, precision
Tensioned wire with a servo U/V axis and programmed offsets skim each contour repeatedly, closing in on the final size.
• TLBJ-40TC — 400 × 500 mm travel
• ±0.005 mm on a Ø10 mm octagon
• Ra 1.2 µm after multiple passes
What the wire cut EDM machine controls
Four things separate a machine that holds tolerance through a long shift from one that drifts: the cast bed, the wire path, the pulse power supply and the way the control handles the cut.

Resin-sand Cast Bed

Frequency-controlled Wire

3rd-gen Digital Pulse Supply

Four-axis Linkage Control
Wire cut EDM machine models
Two fast-wire sizes and one precision medium-wire machine. An EDM machine of this class is judged on the cast bed and the pulse supply, so both are published in the table below. Every unit is commissioned and trial-cut before it ships, and we quote the exact configuration rather than a brochure figure. Both fast-wire models are a cnc wire cut machine on the same control; the difference is the table and the thickness they take.
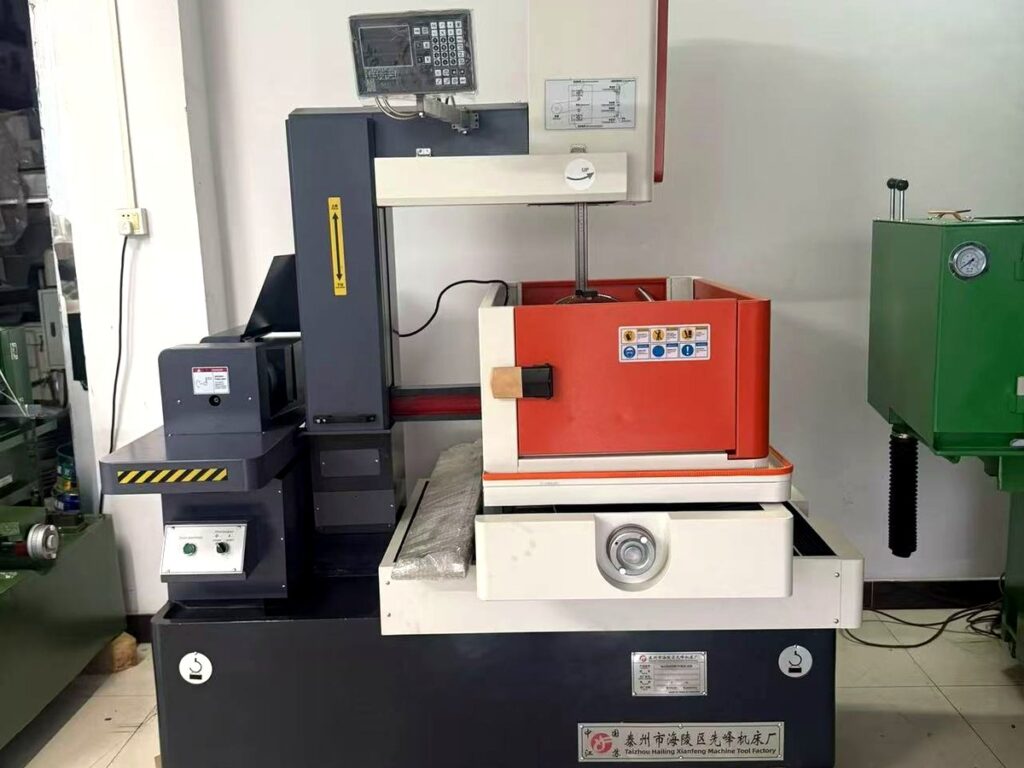
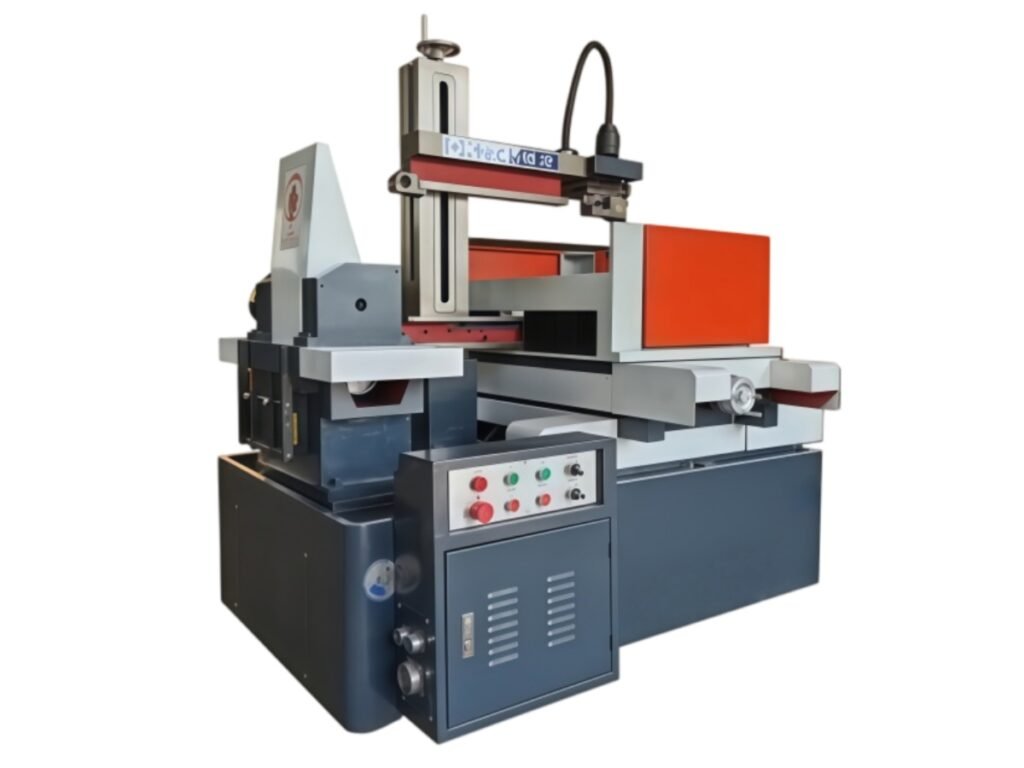
DK7745 Wire Cutting Machine
The largest table in the fast-wire range, for big die plates and components up to 400 mm thick. Handles taper work to ±3° and carries 450 kg on the table.
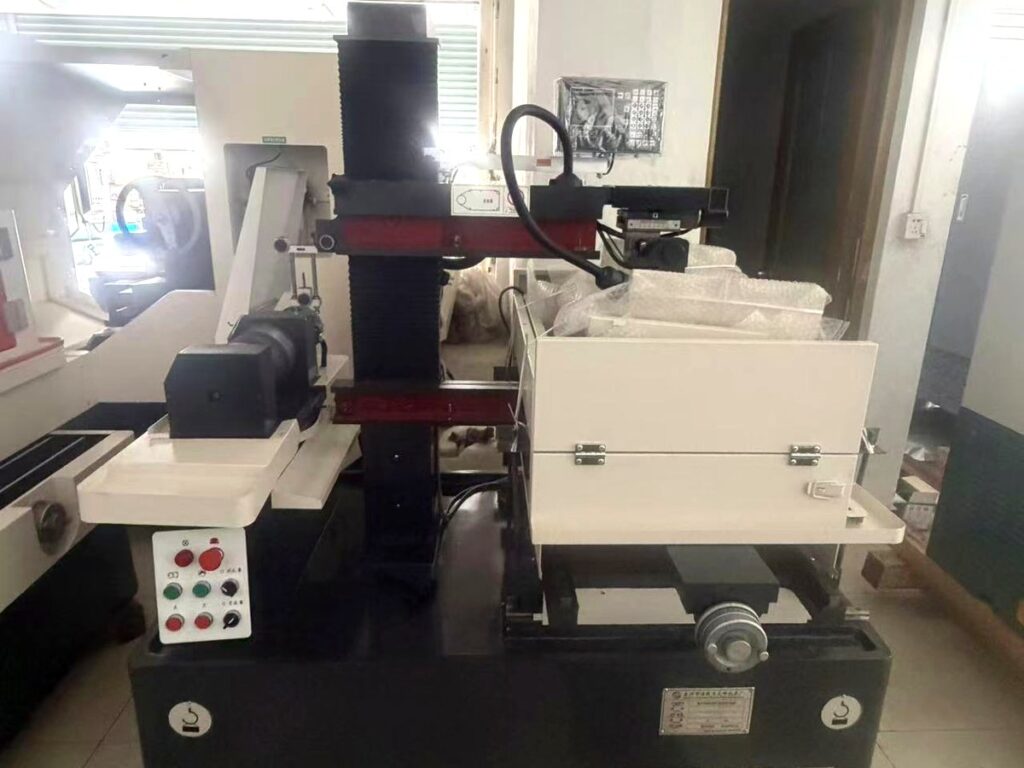
DK7735 Wire Cutting Machine
A compact fast-wire machine for workshop-floor die maintenance and small lot production. Same cast bed and pulse supply as the larger model, in a smaller footprint.
TLBJ-40TC Medium Wire Machine
The precision choice: Taiwan ground ballscrews and H-class linear guides, a 5 µm grating scale, twin-direction wire tensioning and multi-pass cutting down to Ra 1.2 µm.
Wire cut EDM machine specification
Figures below are taken from the manufacturer’s technical sheet for each model. Actual specification follows the configuration you order and the unit we quote.
| Parameter | Value |
|---|---|
| Capacity | |
| Model | DK7745 ±3° |
| Table travel | 550 × 450 mm |
| Max. cutting thickness | 400 mm |
| Table size | 510 × 730 mm |
| Max. cutting taper | ±3° (at 80 mm) |
| Table load capacity | 450 kg |
| Machining performance | |
| Max. cutting efficiency | 100 mm²/min |
| Max. cutting current | 5 A |
| Surface roughness | Ra ≤3.0 µm |
| Machining accuracy | GB7926-2005 |
| Ø10 mm round tolerance | 0.015 mm max. |
| Wire & wire travel | |
| Electrode wire diameter | 0.10–0.20 mm |
| Wire speed | Inverter variable |
| Drum run-out | ≤0.02 mm |
| Wire protection | Stall / limit / break |
| Coolant & power | |
| Power supply | 380 V ±10%, 50 Hz |
| Dielectric tank capacity | 50 L |
| Working fluid | Emulsion paste / water-based |
| CNC control | |
| Control hardware | Dedicated EDM PC |
| Memory / display | 2G / 4G, 15″ LCD |
| Interfaces | USB, LAN, mouse, keyboard |
| Axes | 4-axis linkage |
| Control system | HL control system |
| Programming | Program & control integrated |
| Electrical cabinet | |
| Pulse supply | 3rd-gen digital, 9 combinations |
| Max. current rating | ≤6 A |
| Efficiency per amp | ≥50 mm²/min·A |
| Thick-section efficiency | ≥80 mm²/min at 500–1000 mm |
| Wire loss | ≤0.01 mm per 100,000 mm² |
| Key components | |
| Bed casting | Resin sand, annealed |
| Ballscrew | Beifang precision ball screw |
| Guideways | V-type steel rail |
| Bearings | NSK / SKF |
| Drive motor | Domestic stepper |
| Coolant pump | Weite motor |
| Auto lube pump | Nanjing Biaoya |
| Inverter | Shenzhen make |
| Control cabinet | Original factory |
| Standard equipment | |
| Supplied fixtures | Clamp set, tension wheel, handle |
| Work lamp | 1 × LED |
| Documents | Operation manual, tool kit |
| Parameter | Value |
|---|---|
| Capacity | |
| Model | DK7735 ±3° |
| Table travel | 450 × 350 mm |
| Max. cutting thickness | 400 mm |
| Table size | 500 × 740 mm |
| Max. cutting taper | ±3° (at 80 mm) |
| Table load capacity | 450 kg |
| Machining performance | |
| Max. cutting efficiency | 160 mm²/min |
| Max. cutting current | 8 A |
| Surface roughness | Ra ≤2.5 µm |
| Machining accuracy | GB7926-2005 |
| Ø10 mm round tolerance | 0.015 mm max. |
| Wire & wire travel | |
| Electrode wire diameter | 0.10–0.20 mm |
| Wire speed | Inverter variable |
| Drum run-out | ≤0.02 mm |
| Wire protection | Stall / limit / break |
| Coolant & power | |
| Power supply | 220 V ±10%, 50 Hz |
| Dielectric tank capacity | 80 L, high-pressure |
| Working fluid | Emulsion paste / water-based |
| CNC control | |
| Control hardware | Dedicated EDM PC |
| Memory / display | 2G / 4G, 15″ LCD |
| Interfaces | USB, LAN, mouse, keyboard |
| Axes | 4-axis linkage |
| Control system | AUTOCUT, vertical cabinet |
| Programming | Program & control integrated |
| Electrical cabinet | |
| Pulse supply | 3rd-gen digital, 9 combinations |
| Max. current rating | ≤8 A |
| Efficiency per amp | ≥150 mm²/min·A |
| Thick-section efficiency | ≥80 mm²/min at 500–1000 mm |
| Wire loss | ≤0.01 mm per 100,000 mm² |
| Key components | |
| Bed casting | Resin sand, annealed |
| Ballscrew | Beifang precision ball screw |
| Guideways | V-type steel rail |
| Bearings | NSK / SKF |
| Drive motor | Domestic stepper |
| Coolant pump | Weite motor |
| Auto lube pump | Nanjing Biaoya |
| Cabinet display | Branded 17″ colour |
| Control cabinet | Original factory |
| Standard equipment | |
| Supplied fixtures | Clamp set, tension wheel, handle |
| Work lamp | 1 × LED |
| Documents | Operation manual, tool kit |
| Parameter | Value |
|---|---|
| Capacity | |
| Model | TLBJ-40TC stepper, high precision |
| Table travel | 400 × 500 mm |
| Max. cutting thickness | 300 mm, adjustable |
| Table size | 458 × 578 mm |
| Max. cutting taper | ±3° (at 80 mm) |
| Table load capacity | 500 kg |
| U axis | ±11 mm |
| V axis | ±11 mm |
| Machine structure | |
| Bed casting | Resin sand, annealed |
| Wire tensioning | Bi-directional lateral, adjustable |
| Machining performance | |
| Max. cutting efficiency | 100–120 mm²/min (Cr12 40 mm) |
| Max. cutting current | 6 A |
| Roughness, single pass | Ra ≤2.5 µm |
| Roughness, multi-pass | Ra ≤1.2 µm |
| Machining accuracy | ≤±0.005 mm (Ø10 mm octagon) |
| Wire & wire travel | |
| Electrode wire diameter | Ø0.13–Ø0.20 mm |
| Wire speed | Inverter variable |
| Drum run-out | ≤0.02 mm |
| Wire protection | Stall / limit / break, auto-eject handle |
| Coolant & power | |
| Power supply | 380 V ±10%, 50 Hz |
| Dielectric tank | Semi-enclosed, ≥60 L |
| Filtration | Filter cartridge, 0.01 mm |
| Coolant pump | High-flow, low-pressure |
| Working fluid | Emulsion paste / water-based |
| CNC control | |
| Control cabinet | Autocut stepper MS, vertical cabinet |
| Control hardware | Dedicated EDM PC |
| Memory / display | 2G / 4G, 16G HDD, 17″ LCD |
| Interfaces | USB, LAN, mouse, keyboard |
| Axes | 4-axis linkage |
| Digital readout | 5 µm precision grating scale |
| Electrical cabinet | |
| Pulse supply | 3rd-gen digital, 9 combinations |
| Max. current rating | ≤6 A |
| Thick-section efficiency | ≥80 mm²/min at 500–1000 mm |
| Wire loss | ≤0.01 mm per 100,000 mm² |
| Key components | |
| Ballscrew | Taiwan precision, double-nut ground |
| Guideways | Taiwan H-class linear guide |
| Drive motor | Baoma 90BF 5-phase 10-beat stepper |
| Bearings | NSK / SKF |
| Grating scale | Branded, 5 µm |
| Coolant pump | Pedrollo (Italy) |
| Auto lube pump | Nanjing Biaoya |
| Inverter | Shihlin |
| Wire guide | Diamond eyelet |
| Cabinet display | Branded 17″ colour |
| Standard equipment | |
| Molybdenum wire | 1,000 m / reel included |
| Leveling screws | 4 pcs, original |
| Supplied fixtures | Clamp set, tension wheel, handle |
| Documents | Operation manual, tool kit |
All dimensions in millimetres unless otherwise stated.
Cutting efficiency depends on material, workpiece thickness, wire diameter and parameter set-up; quoted figures are the manufacturer’s reference values.
Accuracy figures follow the GB7926-2005 standard for reciprocating wire-cut EDM machines.
Specifications are typical values for each model and subject to change without notice. Final specification follows the confirmation drawing and quotation.
Tell us the parts you cut and we will confirm the right table travel, cut depth and pass strategy for your work.
Machine photos
Every wire EDM is assembled, aligned and test-cut before it is crated. These are the units in stock and in build — the same models listed in the table above, photographed from the operator’s side. Click any photo to see it full size.
DK7745 fast wire EDM — resin-sand bed, wire drum and control cabinet
The same DK7745 on a clean background, 45° view for the shape of the bed
TLBJ-40TC medium wire — multi-pass head, dielectric tank and flushing
DK7735 — compact fast-wire machine, 350 mm class worktable
Cutting a specific part? Send the drawing or a sample and we will photograph the actual machine and the test cut before it ships — wire path, worktable and control panel.
Request machine photos →Which model fits your part?
The three machines overlap on taper and wire diameter. They separate on table travel, cut depth and how many passes they can put through a contour — which is what ultimately sets the tolerance and the finish.
| Parameter | DK7735 | DK7745 | TLBJ-40TC |
|---|---|---|---|
| Cutting method | Fast wire (HS) | Fast wire (HS) | Medium wire, multi-pass |
| Table travel | 450 × 350 mm | 550 × 450 mm | 400 × 500 mm |
| Table size | 500 × 740 mm | 510 × 730 mm | 458 × 578 mm |
| Max. cut thickness | 400 mm | 400 mm | 300 mm (adjustable) |
| Max. taper | ±3° at 80 mm | ±3° at 80 mm | ±3° at 80 mm |
| Machining accuracy | 0.015 mm (Ø10 mm) | 0.015 mm (Ø10 mm) | ±0.005 mm |
| Surface roughness | Ra ≤2.5 µm | Ra ≤3.0 µm | Ra ≤1.2 µm (multi-pass) |
| Max. efficiency | 160 mm²/min | 100 mm²/min | 100–120 mm²/min |
| Max. current | 8 A | 5 A | 6 A |
| Table load | 450 kg | 450 kg | 500 kg |
| U / V axis | — | — | ±11 mm / ±11 mm |
| Screws & guides | Ball screw, V-type rail | Ball screw, V-type rail | Taiwan ground screw, H-class guide |
| Digital readout | By control | By control | 5 µm grating scale |
| Power supply | 220 V ±10%, 50 Hz | 380 V ±10%, 50 Hz | 380 V ±10%, 50 Hz |
| Best for | Compact die work | Large die plates | Punches, inserts |
Four steps from drawing to quote
Most wire cutting enquiries come down to the same four questions. Answering them up front is what lets us quote a machine that fits, rather than the largest one on the list.
Part size and weight
Thickness
Tolerance and finish
Taper and quantity
Where these machines earn their place
Wire EDM is chosen when the cut has to be square, burr-free and repeatable in already-hardened material — and when a milling cutter simply cannot reach the corner.
Stamping dies & punches
Injection mould inserts
Precision gears & cams
Medical & instrument parts
Wire cut EDM machine questions before ordering
Fast wire cutting (HS-WEDM) uses a molybdenum wire travelling at high speed that is reused across the job, cutting each contour in a single pass. It is the economical choice for hardened die plates, punches and general metal parts where Ra 2.5–3.0 µm is acceptable.
Medium wire cutting (MS-WEDM) keeps the same reciprocating wire principle but adds a servo-driven U/V axis, a tensioned wire system and programmable multi-pass offsets, so each contour is skimmed several times. That brings roughness down to Ra 1.2 µm and accuracy to ±0.005 mm — closing most of the gap to slow-wire EDM at a fraction of the price.
DK7735 — workpieces within a 450 × 350 mm travel, where budget and footprint matter more than table size.
DK7745 — larger die plates, 550 × 450 mm travel, and plates up to 400 mm thick.
TLBJ-40TC — parts that need tight tolerance and a fine finish: punches, inserts, precision cams. Multi-pass cutting to Ra 1.2 µm at ±0.005 mm, with a 300 mm adjustable depth.
All three models achieve ±3° taper at an 80 mm workpiece thickness. The taper is programmed through the control software and executed by the U/V axis arrangement, so draft angles, clearance angles and taper-cut dies are produced directly from the part drawing — no separate operation and no re-setup.
DK7745 and TLBJ-40TC run on 380 V ±10%, 50 Hz three-phase power. DK7735 is supplied in a 220 V ±10%, 50 Hz configuration. Please confirm your plant voltage when ordering so the correct transformer and control cabinet configuration are prepared before shipment.
Yes. Every machine ships with the operation manual, tool kit, fixtures and a documented commissioning checklist. We support programming, parameter set-up for your material and thickness, and spare-part supply.
Remote guidance is available for first-article trials, and on-site commissioning can be arranged for multi-machine orders.
Yes. We can adapt the control cabinet to your plant voltage, provide the control interface in your preferred language, and quote custom work-holding fixtures, extended table sizes and additional coolant tank capacity. Send your workpiece drawings and plant conditions and we will confirm what is feasible before quoting.
They describe the same machine. EDM names the process, wire cut names the tool, and CNC names the control that moves the table. A wire edm machine sold today is a cnc wire cut machine by definition.
Up to plus or minus 3 degrees at 80 mm on the fast-wire models, with the U and V axes programmed. Variable taper is set in the same programme as the contour.
A level floor is enough for the fast-wire sizes; the medium-wire machine is happier on a strip foundation because the finish depends on the machine not moving. We send the footprint and weight before delivery.
Tell us the part, and we will confirm the machine
Send the drawing with the plate thickness, the tolerance and the finish you need. We will confirm the model, the configuration, the price and the lead time — and say plainly if a different machine suits you better. If you are comparing an EDM surface finish chart from another builder, send it across and we will map the Ra figures to the passes our machines actually run.